Robots flawlessly repeat mistakes. That won’t happen with our solutions. Find out more about stable processes here!

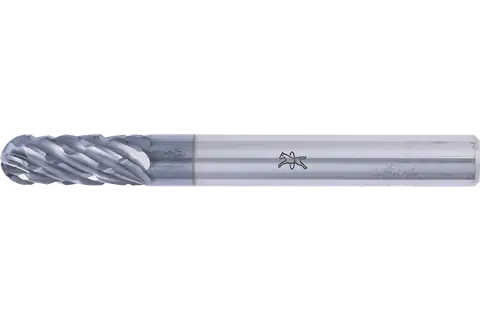
Tungsten carbide burrs for high performance, ALLROUND HC-FEP, cylindrical shape with radius end WRC

Tungsten carbide high-performance burr ALLROUND cylindrical with radius end WRC dia. 06x16 mm shank dia. 6 mm HICOAT coated for steel

WRC 0616/6 ALLROUND HC-FEP
Item number:
21001082
EAN:
4007220771082
New
Technical information
Tungsten carbide high-performance burr ALLROUND cylindrical with radius end WRC dia. 06x16 mm shank dia. 6 mm HICOAT coated for steel

Cut
ALLROUND HC-FEP
Dia. external
6 mm
Dia. shank
6 mm
Length, cut
16 mm
Length, total
55 mm
RPM, grey cast iron, white cast iron
24000 - 58000 RPM
RPM, hard non-ferrous metals
13000 - 40000 RPM
RPM, hardened, heat-treated steels over 1,200 N/mm²
13000 - 32000 RPM
RPM, rust and acid-resistant steels
24000 - 40000 RPM
RPM, soft non-ferrous metals
24000 - 48000 RPM
RPM, steels up to 1,200 N/mm²
24000 - 48000 RPM
Packaging unit
1 piece
Description

High-performance cut ALLROUND with HICOAT coating HC-FEP is characterized by its high degree of hardness and wear resistance. It enables effective chip removal through improved anti-adhesion characteristics and is highly temperature-resistant. It allows for a longer tool life and use at higher cutting speeds in comparison with uncoated burrs.

Cylindrical burr with radius end according to DIN 8032. Combination of cylindrical and ball-shaped geometries.

Special features
  • Significantly better stock removal rate than burrs with a conventional cross cut.
  • Saves time and money thanks to its very high stock removal rate on key materials.
  • Comfortable working with reduced vibration and less noise.
  • The highly accurate concentricity enables impactfree working without creating chatter marks. This considerably reduces wear on the tool and tool drive.
Recommendations for use
  • To prevent vibrations, place the tools on powerful drives with an elastically supported spindle wherever possible.
  • Observe the recommended rotational speeds.
  • To ensure costeffective use of burrs, use a higher rotational speed and cutting speed. Use burrs with a shank diameter of 6 mm with drives with a power output from 300 watts.
Safety notes
  • The very high stock removal rate can cause discolouration on the shank. This does not constitute a safety risk.
Materials that can be worked
Annealed cast iron
Black annealed cast iron (GTS, GJMB)
Brass
Bronze
Case-hardened steels
Cast iron
Cast steel
Copper
Grey/nodular cast iron (GG/GJL, GGG/GJS)
Hard aluminium alloys
Hardened, heat-treated steels over 1.200 N/mm² (< 38 HRC)
Hard non-ferrous metal
Soft non-ferrous metal
Stainless steel (INOX)
Steel
Steel, cast steel
Steel materials with a hardness > 54 HRC
Steels over 700 N/mm² (> 220 HB)
Steels up to 1,200 N/mm² (< 38 HRC)
Steels up to 700 N/mm² (< 220 HB)
Titanium
Titanium alloys
Tool steels
White annealed cast iron (GTW, GJMW)
Zinc
Applications
Cutting out holes
Deburring
Leveling
Milling
Milling out
Surface work
Work on weld seams
Drive types
Automated centres
Drive spindle
Flexible shaft drive
Straight grinder
Tool machine
Downloads

PFERD TOOLS Newsletter subscription

Register here free of charge for our PFERD TOOLS newsletter and receive all the latest news on products, services and promotions from the world of PFERD TOOLS on a regular basis.